Description
Product Overview
Spirax Sarco Gasket Set B, G is a dedicated replacement seal package engineered for two-port globe control valves across the Spira-trol K and L series. Installed during routine disassembly or scheduled maintenance, this kit replaces degraded bonnet and seat gaskets to eliminate external flange leakage and prevent internal seat bypass in high-temperature steam and fluid pipelines.
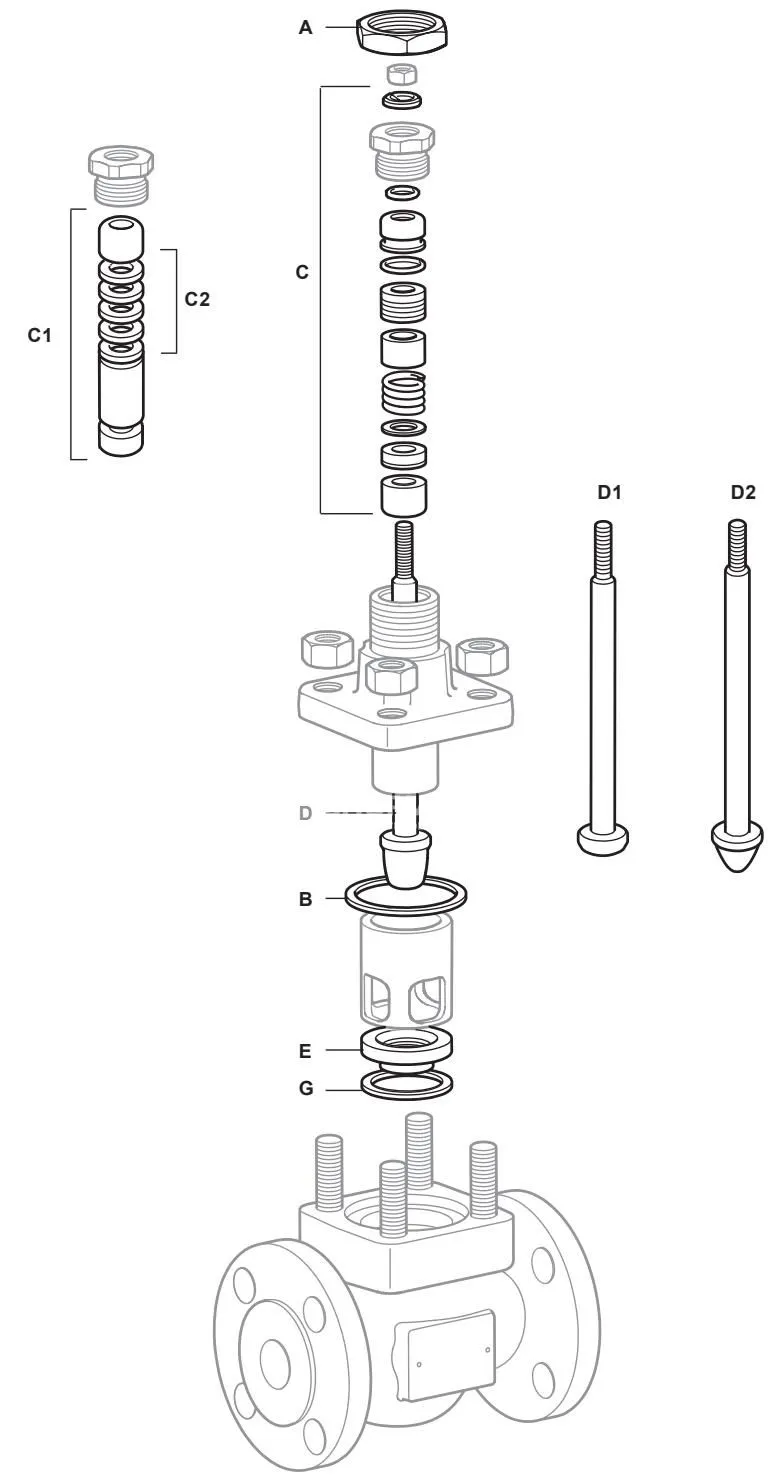
Spirax Sarco maintenance protocols specify that whenever a valve bonnet is removed or internal trim components are serviced, all soft seals and gaskets must be discarded and replaced. The non-bellows gasket set supplies the critical static sealing interfaces designated as Part B (bonnet gasket, Item 4) and Part G (seat gasket, Item 7), restoring factory pressure containment standards.
Key Features
- Comprises both primary static seals for non-bellows Spira-trol valves: bonnet gasket (B) and seat gasket (G).
- Spiral wound composite construction combining AISI 316L stainless steel windings and high-purity exfoliated graphite filler.
- Engineered to fit 4 standardized Spira-trol body envelopes across sizes DN15 to DN100, plus large-bore unbalanced models DN125 to DN300.
- Delivers high recovery and compressive strength under variable thermal cycling up to 400 °C (SG iron, carbon steel) or 538 °C (stainless steel body limits).
- Guarantees seat ring alignment without pinching the cage or damaging internal body recesses.
Technical Specifications
| Parameter | Specification Details |
|---|---|
| Product Designation | Gasket set (Non-bellows sealed) |
| Spare Part Identification Codes | B (Bonnet gasket), G (Seat gasket) |
| Host Valve Series | Spira-trol K series (KE43, KE61, KE63, KE71, KE73, KEA) and L series (LE31, LE33, LE43, LE63, LEA) |
| Compatible Host Size Range | DN15, DN20, DN25, DN32, DN40, DN50, DN65, DN80, DN100, DN125 to DN300 (unbalanced) |
| Standard Gasket Construction | 316L stainless steel spiral wound with graphite filler |
| Optional Gasket Construction | PTFE (available on specific EN valve configurations) |
| Maximum Operating Temperature | 400 °C to 538 °C (governed by valve body and bolting material ratings) |
| Cold Hydraulic Test Compatibility | Up to 60 bar g (KE43, KE63), 75 bar g (KEA63), 77 bar g (KEA43), 37.5/38 bar g (KE71, KE73), 24 bar g (PN16) |
| Ordering Requirement | Specify full valve description and body nameplate date code (size, series, trim, Cv/Kvs) |
Applications
- Routine annual inspection and preventive maintenance of Spira-trol globe control valves.
- Re-sealing the valve body-to-bonnet joint whenever replacing PTFE chevron packings or high-temperature graphite stem seals.
- Valve trim refitting, seat renewal, or conversion kit installation (including Steam-Tight C trim retrofits).
- Rectifying external stem/bonnet joint leaks caused by gasket relaxation, bolting undertorque, or thermal shock.
- Eliminating internal seat ring bypass leakage in steam, condensate, gas, and liquid process lines.
Installation and Maintenance Procedures
Before undertaking gasket replacement, depressurize connecting pipework, drain all media, and isolate the control actuator. Follow the step-by-step procedure detailed in Spirax Sarco IM-S24-42:
- Remove the actuator assembly and loosen bonnet fasteners (bonnet nuts 27 or bolts on LE valves).
- Withdraw the bonnet assembly (2) and carefully remove the old bonnet gasket (B / 4). Discard the used gasket immediately.
- Lift out the seat retaining cage (5) and seat ring (6). Extract the seat gasket (G / 7) from the lower body recess and discard it.
- Clean all gasket surfaces thoroughly. Remove any residual graphite residue from the body seat recess and bonnet mating faces.
- Position a new seat gasket (7) squarely in the body seat recess, followed by seat ring (6) and cage (5). Ensure cage flow windows face downward.
- Place a new bonnet gasket (4) onto the body face. Reinstall the bonnet and stem assembly, keeping the plug centered in the seat.
Recommended Tightening Torques
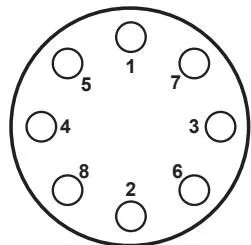
To ensure uniform gasket compression and avoid plug/seat misalignment, tighten bonnet nuts gradually in opposite pairs across diameters following the sequence shown in Fig. 6 (4-hole) or Fig. 7 (8-hole). Increment torque through 10%, 20%, 40%, 60%, 80%, and finally 100% of the target value. Cycle the valve stem after each tightening phase to verify smooth, unhindered travel.
Bonnet Bolting Torques (DN15 to DN100)
| Valve Size | Standard Versions (except Steam-Tight C) | Steam-Tight C Options | LE Series (Cast/Carbon/Stainless) | LEA, KE, KEA Series |
|---|---|---|---|---|
| DN15 - DN25 (½” - 1”) | 50 N m | 30 N m | 70 N m | 100 N m |
| DN32 - DN50 (1¼” - 2”) | 70 N m | 50 N m | 90 N m | 130 N m |
| DN65 - DN80 (2½” - 3”) | 130 N m | 130 N m | 110 N m | 130 N m |
| DN100 (4”) | 100 N m | 100 N m | 110 N m | 130 N m |
Bonnet Bolting Torques (DN125 to DN300 Unbalanced)
| Valve Size | KE Series Body | KEA Series Body |
|---|---|---|
| DN125 | 203 N m | - |
| DN150 | 211 N m | 245 N m |
| DN200 to DN300 | 265 N m | 365 N m |